Updated on October 29, 2026
PEEK is a high-performance thermoplastic valued for high temperature resistance, chemical inertness and biocompatibility, widely used in medical, semiconductor and aerospace CNC components. PEEK has special machining risks including thermal buildup, melting and internal stress. This guide covers grades, tolerance rules, cooling strategy and medical compliance notes for PEEK CNC prototypes.
Definition
PEEK (Polyetheretherketone) is a high-performance thermoplastic polymer widely used for precision components that demand high temperature resistance, chemical stability, mechanical strength and low outgassing. PEEK machining is the subtractive manufacturing process that cuts solid PEEK stock into custom parts via CNC milling, turning and drilling.
Unlike common plastics such as POM or nylon, PEEK retains mechanical properties at continuous operating temperatures up to 260°C. It is a top choice for medical, aerospace and automation applications. PEEK CNC prototypes are frequently used for functional testing when standard engineering plastics cannot meet thermal or chemical requirements.
How It Works
PEEK CNC machining follows a controlled workflow to avoid melting, delamination and internal stress:
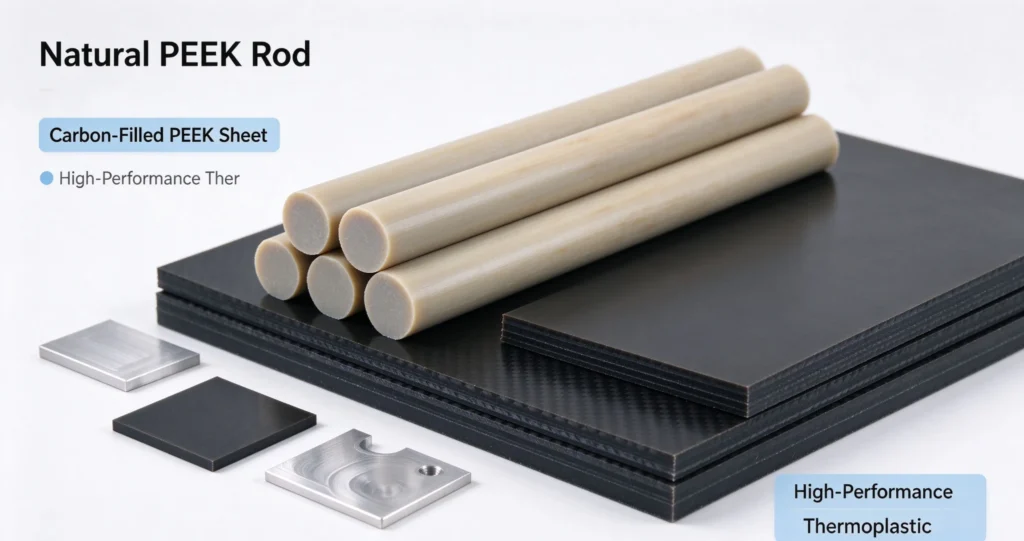
- Material selection: Choose natural PEEK, carbon-filled or glass-filled PEEK grades based on stiffness and wear needs.
- Blank preparation: Use stress-relieved PEEK rod or sheet to reduce warping after cutting.
- CNC programming: Set conservative cutting speed, feed rate and depth of cut. Sharp, polished cutting tools are required.
- Machining: Milling, turning and threading; compressed air cooling is preferred instead of liquid coolant.
- Deburring & post-processing: Gentle deburring; avoid excessive heat on edges.
- Dimensional inspection: Verify tolerances, especially for thin walls and small features.
Heat buildup is the biggest risk in PEEK machining. Even localized overheating can cause surface melting and dimensional shift.
Key Parameters
Critical factors that control PEEK part quality and manufacturability: PEEK grade, cutting speed, feed rate, tool type, cooling method, wall thickness and tolerance requirement.
表格
| Factor | PEEK Machining | POM / Nylon Machining |
|---|---|---|
| Heat resistance | Up to 260°C continuous use | Below 120°C typically |
| Tool requirement | Sharp polished carbide tools | Standard HSS or carbide tools |
| Cooling | Dry air cooling recommended | Liquid coolant acceptable |
| Risk | Melting, stress warpage, chipping | Easy to cut, risk of deformation |
| Cost of raw material | High | Low |
| Best use case | High-temperature, chemical-resistant precision parts | General-purpose low-cost plastic components |
Pros & Cons
✅ Advantages
- Outstanding thermal, chemical and hydrolysis resistance
- Excellent strength-to-weight ratio and low friction
- Biocompatible grades available for medical component prototyping
- Stable performance under repeated thermal cycling
- Low smoke and low outgassing for aerospace environments
❌ Limitations
- Very expensive raw material
- Prone to thermal melting and stress-induced warping
- Filled PEEK (carbon/glass) abrades cutting tools quickly
- Thin walls and fine features have higher failure risk
- Slow machining speed raises processing cost
PEEK is only selected when ordinary plastics cannot satisfy the working conditions.
Typical Applications
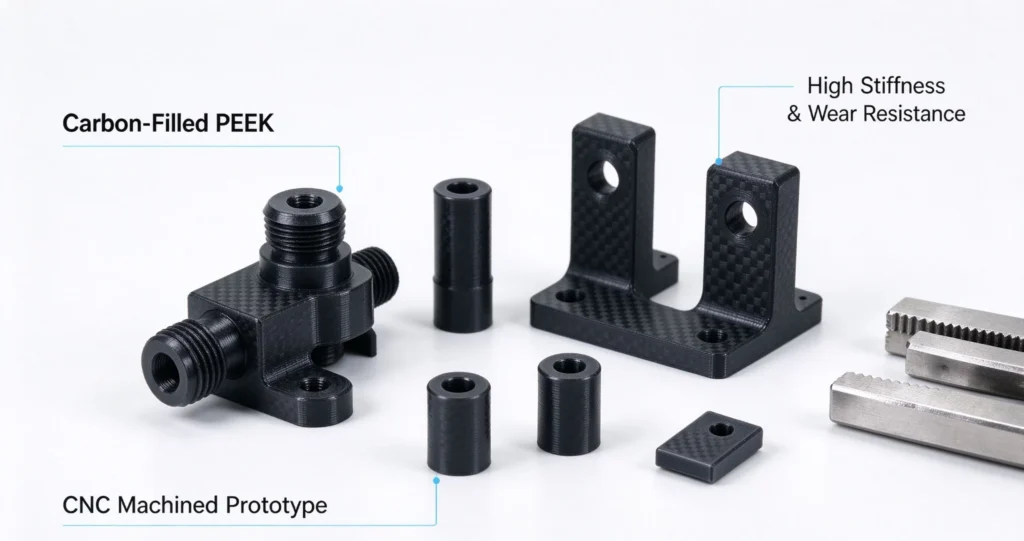
- Aerospace: Lightweight structural spacers, insulator brackets and fluid component prototypes
- Medical: Surgical fixture components, instrument housings and non-implant test prototypes
- Industrial automation: High-temperature bearing sleeves, wear-resistant guide blocks and sensor insulators
- E-bike & mobility: High-load, heat-resistant spacer and bushing parts
We deliver custom PEEK CNC machined parts and low-volume PEEK prototypes with strict dimensional control.
Design & Machining Tips
- Avoid thin walls thinner than 0.8 mm; thicker sections reduce warping risk
- Add generous radii to inside corners to prevent stress cracking
- Keep hole depth and diameter ratio reasonable; deep small holes are hard to machine cleanly
- Clearly specify PEEK grade: natural, carbon filled, glass filled or medical grade
- Do not design sharp internal edges; sharp corners concentrate residual stress
- Mark critical tolerance features on drawings and allow extra inspection time
- Work with a machinist experienced in high-performance plastics to set proper cutting parameters
Early DFM review helps reduce thermal distortion and scrap for expensive PEEK blanks.
FAQ
Q: Is PEEK suitable for medical implant parts?
A: Medical-grade PEEK (PEEK 450G) is biocompatible and widely used for non-permanent medical devices. Implant-grade PEEK requires strict material traceability and certification.

Q: Why is PEEK tricky to machine?
A: PEEK has low thermal conductivity. Heat accumulates at the cutting zone, causing melting, built-up edge and residual stress inside the part.

Q: What tolerance can be held on CNC PEEK parts?
A: Practical tolerance ±0.10 ~ ±0.15 mm. Tighter tolerances are possible but require slow cuts and fixture support.

Q: Do PEEK parts need post-annealing?
A: Annealing relieves internal machining stress for high-precision PEEK parts that require stable dimensions.


